


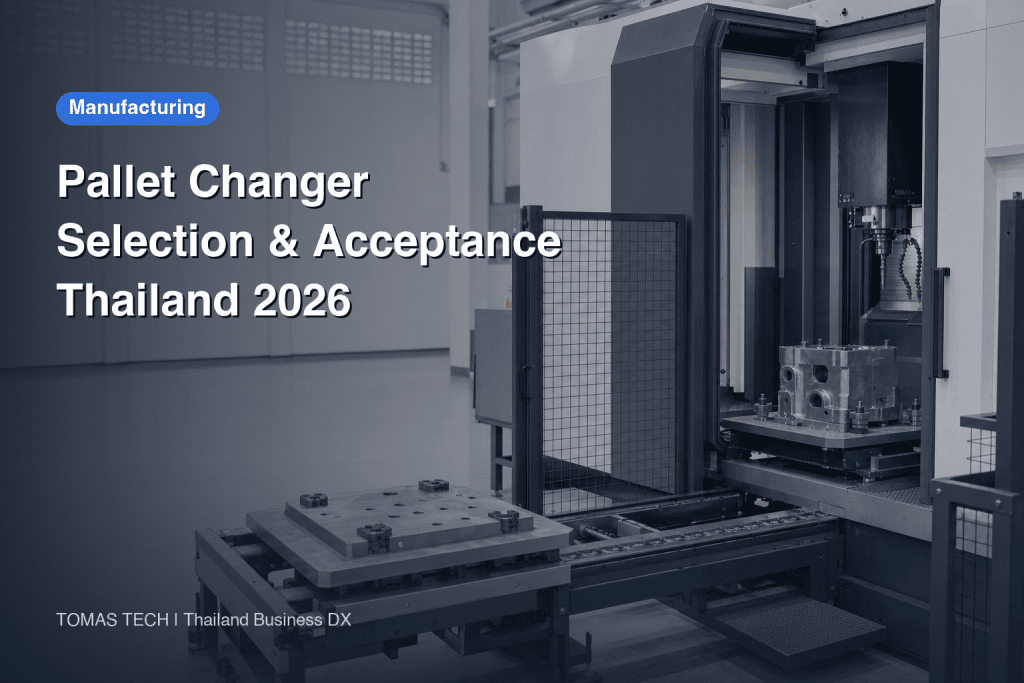
When selecting an automatic pallet changer (APC) for a machining cell in Thailand, the first comparison should be the causes of spindle downtime, not a catalogue changeover time. Where will the next workpiece be fixtured? Who will prepare it? What signals can the existing CNC exchange with an external device? An APC swaps a workpiece and fixture together while the next pallet can be prepared outside the machine. It delivers value only when fixtures, tools, programs, safety controls and recovery procedures support the whole sequence. This guide compares a two-pallet APC, a pallet pool and a multi-machine cell, then turns the choice into a request for proposal (RFP) and measurable factory and site acceptance tests (FAT/SAT).
Start with measured reasons for machine stoppage
Separate unloading, fixturing, locating, clamping, tool checks, program checks and first-piece inspection. An APC can move much of the workpiece setup outside the spindle enclosure; it cannot eliminate waiting for a missing tool or approval from inspection. Record the time, reason, owner and restart condition for representative parts over several production days. Makino describes its integral APC as allowing one pallet to be set up while the other is machined; that is the mechanism to test in your own process, not a universal productivity percentage. Makino Slim3n APC.
If machining is long enough to prepare the next pallet, a two-pallet APC may be enough. If short, mixed jobs need to wait in a planned sequence, a pool and job management may be more useful. If preparation takes longer than machining, the spindle will still wait even with two pallets. Compare this opportunity against improvements in CNC production preparation and machine-tool monitoring. Count good parts per constrained hour, not only the nominal motion time of the changer.
Compare three different architectures
Two-pallet APC
A two-pallet APC alternates a pallet in the machining chamber with one at the outside setup station. It is a strong candidate when one CNC processes a relatively stable family of fixtures and the operator can prepare the next pallet while machining continues. Verify the exact CNC model, serial number, controller generation and installed options before assuming OEM integration or retrofit compatibility. Makino describes both standalone and APC configurations for its D500, including a possible later upgrade; that statement belongs to that model, not every machine. Makino D500.
The limitation is that only one next pallet is ready. If it is late, the spindle waits. For mixed production, establish how pallet ID selects the part program, fixture, work offset, tooling and inspection instruction. Haas documentation illustrates pallet scheduling and program assignment on its APC. Use it as an example of the required workflow, while confirming the actual control behavior with the chosen OEM. Haas APC operator supplement.
Pallet pool
A pool stores several prepared pallets and feeds them in a planned order. It can support mixed jobs and longer periods of operation, provided that jobs are genuinely ready. Compare setup stations, pallet return routes, job priority changes, tool life, finished-part accumulation and restart after an alarm, rather than only counting stations. Makino distinguishes circular pools from larger handling systems serving more than one machine. Makino Pallet Automation.
Measure how long it takes to make each pallet genuinely production ready: material, clamping, datum check, program version, available tools and drawing revision. More empty pallet stations cannot extend unattended time. More work in process also makes physical and digital identification more important. Decide whether barcodes or RFID are needed from the risk of a wrong job, then define exactly when a scan is required.
Multi-machine cell
A shared cell routes pallets between multiple CNCs, a setup station and possibly measurement or washing equipment. It can allocate work to available machines, but a common handling fault can affect the entire cell. Confirm pallet interfaces, payload, datum, fixtures, tools and programs across machines before deciding on a shared transporter. A robot placing bare parts into a machine is a different design problem from exchanging a fixtured pallet; compare it separately in our guide to CNC machine tending.

| Decision point | Two-pallet APC | Pallet pool | Multi-machine cell |
|---|---|---|---|
| Main aim | Parallel machining and setup | Queue several prepared jobs | Route work among machines |
| Control unit | Two pallet identities | Pallets, jobs and sequence | Pallets, machines and shared handling |
| Key constraint | Next pallet not ready | Tools and WIP management | Common faults and ownership |
| Check first | CNC interface | Setup station and job data | Interfaces between all machines |
Check the existing CNC before ordering
For a retrofit, collect the machine serial number, controller and software versions, installed options, electrical diagrams, spare I/O, external M-code facilities, door and clamp circuits, service access and warranty conditions. A cabinet photograph alone does not prove compatibility. Haas documents an M-code/MFIN accessory interface and lists APC READY kits in its applicable-kit list; it is evidence for those Haas configurations, not a specification for other CNC brands. Haas M-FININ option.
Make a signal and responsibility table: who confirms spindle stopped and axes in a safe position; who verifies the door, pallet presence, unclamp and clamp; who confirms the transporter has cleared the machine; and what happens on a timeout. Define sensor owner, message direction and safe state for every step. A simple start/finished handshake is rarely enough to recover safely from an interrupted transfer. If the existing interface has not been surveyed, price the survey separately and state how design changes affect cost and schedule. Ask the machine OEM to confirm permitted modifications, backup and restoration of NC/PLC software, and any effect on warranty.
Prove the pallet, fixture and workpiece fit as a system
Check combined mass and center of gravity of pallet, fixture, clamps, raw stock and finished part. Draw the maximum height and overhang throughout the transfer path, not only at the final machining position. Check crane and forklift access, setup ergonomics, guarding clearance and maintenance space. Test both the heaviest offset load and the lightest load. A nominal payload limit does not by itself resolve center-of-gravity or interference limits.
Machining quality depends on repeatable seating and datums. Inspect locating pins, datum faces, clamp force, air blow, chip removal and coolant paths. Rather than compare a single repeatability number in brochures, exchange the actual pallet repeatedly and measure critical part characteristics under the same fixture and measurement procedure. Include cold start and sustained operation. Group part numbers by common datum and fixture, adaptable fixture, and dedicated fixture. Every dedicated fixture adds capital, storage and change-control work.
Treat pallet identity, NC program and tools as one job
A perfectly clamped pallet can still produce scrap if the wrong program starts. Define each job through pallet ID, part number, operation, fixture revision, program revision, work offset, required tools and inspection instruction. Specify checks at setup completion, before transfer and before cycle start. On a stop, retain enough state to identify the actual pallet location, last completed operation and disposition of the partly machined part.
Tool wear, spare tools, chips, coolant and first-piece approvals can stop a night shift even if many pallets are loaded. Do not assume an APC alone enables unattended machining. On abnormalities, hold a safe state and give the responsible person a clear diagnosis rather than automatically restarting. If MES or ERP integration is planned, first make pallet ID and job state reliable at the equipment. Record start, finish, stop reason, good and rejected quantity, and program version as events. Those records also support machine-tool monitoring.

Engineer safety and abnormal recovery alongside the normal cycle
Transfer brings moving mass, pinch points, machine doors and human setup into the same area. Design guards, interlocks, emergency stops, maintenance modes, energy isolation and restart from the actual risk assessment. ISO 16090-1:2022 covers machining centers and integral workpiece transfer devices within its scope. Citing a standard number does not certify a particular installation; ask the supplier for applicable hazards, safeguards and verification records. ISO 16090-1:2022.
Test power loss during transfer, a pallet not seated, failed clamp, door fault, chip-obscured sensor, NC alarm, lost upper-level communication and manual extraction. For each, define the displayed condition, physical pallet location, allowed manual actions and conditions for restarting. Haas’s maintenance schedule includes cleaning chips around its APC receiver and clamp switch and inspecting locating and wiping components. Use the chosen OEM’s own maintenance intervals, while ensuring contamination is addressed in trials and routine checks. Haas VMC maintenance schedule.
Include plant layout and utilities in the quotation
Overlay setup space, pallet storage, inspection bench, crane travel, forklift routes and cover-removal space on the factory drawing. Confirm floor loading, anchoring, leveling, air, power, network, coolant, chips and emergency access. For a retrofit, include when the existing line will stop for delivery and commissioning. Confirm the actual machine and its modification history on site; drawings from headquarters can differ from the installation in Thailand. Ask bidders to show the boundary between imported equipment, locally fabricated items, machine modifications and site services.
Calculate payback from net good output
For each representative job, measure current spindle stoppage, stoppage remaining after automation, setup labor, good-part output and feasible night operation. Confirm downstream demand can absorb extra good parts. A simple annual benefit is additional contribution margin plus genuinely avoided overtime, outsourcing and rework only where these savings are not already included in that margin; subtract recurring maintenance, energy, software, replacement spares and support. One-time capital expenditure includes the changer, initial fixtures and pallets, safety, CNC modification, installation, FAT/SAT, initial training and production interruption. Do not count a benefit or cost twice.
As an illustrative calculation, suppose the spindle stops 90 minutes per day; 50 minutes relate to setup; 35 of those minutes can move outside; and the exchange and checks add 10 minutes. The net opportunity is 25 minutes, not 90. This is an example of arithmetic, not a quoted performance or Thailand market price. Replace every input with measured factory data, then test sensitivity to setup readiness, alarms, tool availability, mix and demand. If another process is the bottleneck, additional spindle hours may have little shipment value.
Write an RFP that can be accepted or rejected objectively
First define the initial part family and explicitly exclude prototypes, unusual weights or very rare jobs where they would make the first system unnecessarily complex. State how future expansion is reserved: pallet storage, spare I/O, interface and software licence. Compare an APC retrofit with a replacement machine when the existing machine’s supportability, remaining life or warranty is uncertain.
Provide the CNC identification, part and fixture drawings, minimum and maximum loads, production sequence and site layout. Define output using real loaded pallets and good parts, not only an empty-pallet transfer time. Specify NC/PLC modifications, signal list, pallet ID, job selection, data outputs, each operating mode, guarding, abnormal recovery and maintenance. Request line-item pricing for equipment, fixtures, safety, control changes, upper-level integration, delivery, installation, FAT, SAT, training, warranty and spares. Name the responsible party for every interface among CNC OEM, APC supplier, integrator and plant maintenance team.

FAT: find defects before shipment
At the supplier site, run representative fixtures and workpieces where possible, or simulate mass, center of gravity and envelope while listing what SAT must still prove. Test empty and loaded exchanges, repeated cycles, job sequence changes and planned and unplanned stops. Deliberately try a mismatched pallet ID and program. Verify that failed seating, clamp, door closure, sensor and communication prevent unsafe progression. Record emergency-stop holding and recovery.
For each RFP requirement, write a traceability row with test method, acceptance criterion, result, log, defect owner and retest date. Define whether exchange time is pure mechanism motion or time from completion of one machining cycle to restart of the next. These are different metrics. If FAT uses simulated CNC signals, leave the real CNC interface open for SAT; do not mark it accepted by inference. Check that restoration of power or sensors cannot cause an unexpected restart.
SAT: prove the actual machine, part and shift can operate
At the Thailand site, verify floor, power, air, network, machine leveling and guarding, then connect the real CNC and test its door, clamp, axes, offsets, tools and programs. Progress from manual cycle to one automatic exchange, repeated cycles, mixed jobs, a normal shift and the planned night condition. The RFP should set the number and duration of cycles from production risk rather than copy a generic figure.
Measure important dimensions and good output using normal factory metrology. Train operators and maintenance separately; have each person demonstrate setup, fault diagnosis and recovery. Deliver NC/PLC/HMI backups, electrical and pneumatic drawings, signal table, spares, maintenance checklist and version-controlled instructions. Provide the Thai-language instructions needed for the people on the shift. Installation and first motion are milestones; acceptance follows demonstrated quality, repeatability, recovery and operator competence.
Five questions for supplier comparison
- Which compatibility points have been confirmed on the identified CNC, and which remain unknown?
- How will pallet, fixture, workpiece, tools and program be matched before a cycle starts?
- How will operators recover from power loss, failed clamping and interrupted transfer?
- Which tests use real hardware at FAT, and what remains for SAT?
- Who owns modifications, warranty effects and fault response at every supplier boundary?
Compare written drawings, signal lists and test plans, not just a claimed number of APC installations. Ask whether references match the control generation, load, product mix and service location of your factory.
Frequently asked questions
What determines automatic pallet changer cost?
Architecture and station count matter, but so do CNC changes, fixtures, pallets, guarding, floor works, data integration, FAT/SAT and local support. Use the same RFP and compare scope line by line; overseas product prices are not installed prices in Thailand.
Can an APC be retrofitted to an existing machining center?
It depends on the serial number, control and options, door and clamp circuits, OEM permission and available space. Request a joint site survey with the machine OEM and automation supplier before ordering.
Should we choose two pallets or a pallet pool?
Two pallets suit a simple sequence when the next job is prepared during machining. A pool helps when several jobs must queue or be reprioritized. Neither replaces tools, inspection or operator readiness.
Does an APC guarantee unattended running?
No. Tool life, chips, coolant, measurement, material, abnormal notifications, fire and safety measures, and a defined response team all matter. State the eligible jobs and unattended hours in the RFP and verify them at SAT.
What is the difference between FAT and SAT?
FAT is the supplier-site test before shipment; SAT is acceptance at the actual factory with the actual CNC, parts and personnel. Keep all simulated FAT conditions open until measured on site.
Conclusion
Select a pallet changer by measuring stoppage, choosing the architecture that matches the job flow, then specifying CNC connections, fixturing, safety, job identity and recovery. Compare quotations on equal scope and verify both normal and abnormal operation at FAT and SAT.
If you are still checking retrofit feasibility or preparing an RFP for a Thai machining cell, TOMAS TECH can help organize the machine data, representative parts and test requirements. Contact TOMAS TECH.


